


 English
 中文


When we design a photovoltaic cable extrusion line, we do not look at the extruder as a single machine. We look at the whole Production Process: material feeding, melting, extrusion, forming, cooling, traction, take-up, and the way operators control each step. This is especially important for solar Cable Production, where stable insulation thickness, smooth surface quality, dimensional consistency, and continuous production all matter.
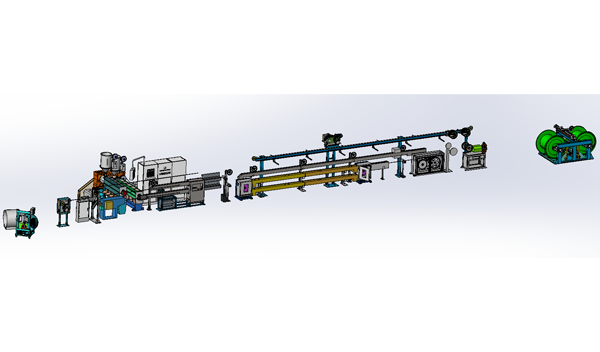
Our 80+100 Photovoltaic Extruder Production Line is developed for photovoltaic wire and cable manufacturing. The line uses two extrusion units with different nominal sizes and coordinates them through the production process. Depending on the cable structure and process requirements, the equipment can be configured for different extrusion materials, product dimensions, production capacities, and factory layouts.
At Wuxi Shuochuan Electromechanical Equipment Manufacturing Co., Ltd., we focus on practical equipment rather than complicated descriptions. We integrate R&D, manufacturing, and sales, and we have obtained more than ten utility model patent certificates. Our approach is simple: understand what the customer needs to produce, select a suitable line configuration, test the equipment before shipment, and make the production process easier for the operator to manage.
This page explains how we approach the 80+100 photovoltaic extrusion Production Line, what the equipment does, where it can be used, what buyers should check before placing an order, and why the complete line matters as much as the extruder itself.
1. What Is an 80+100 Photovoltaic Extruder Production Line?
The name “80+100” generally refers to a production line equipped with two extrusion units with different nominal extruder sizes. In a real production project, however, the model number is only one part of the equipment selection. The correct configuration also depends on the cable structure, insulation or sheath material, target dimensions, production speed, cooling requirements, take-up method, and the customer's workshop conditions.
For photovoltaic cable manufacturing, the extrusion process needs to be controlled carefully. The polymer material is fed into the extruder, heated and plasticized, and then pushed through a die to form a continuous layer around the conductor or previous cable layer. After extrusion, the product passes through cooling and sizing stages before traction and take-up.
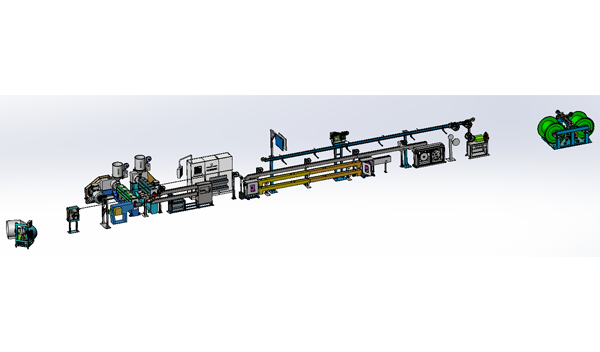
When two extrusion units are used, they can be arranged to meet the required product structure. For example, a production process may require different extrusion stages for different layers or materials. The exact arrangement should be confirmed according to the customer's cable design rather than assuming that every 80+100 line has the same configuration.
That is one reason we normally confirm product specifications before production. We need to understand what the customer is making before deciding how the equipment should be configured.
Typical process flow
Material feeding → Extrusion → Die forming → Cooling → Traction → Inspection → Take-up
For a double-layer or multi-stage product, additional extrusion and forming stages may be incorporated into the line. The purpose is to keep the whole process coordinated, so the operator does not have to treat every machine as an independent unit.
For photovoltaic cable manufacturers, this integrated approach is useful because a stable extrusion process can reduce unnecessary manual adjustment and make production easier to monitor.
2. How the Photovoltaic Cable Extrusion Process Works
It is easy to think of extrusion as simply “melting plastic and putting it around a wire.” In practice, several things happen at the same time. Material temperature, screw movement, melt pressure, die condition, cooling, line speed, and take-up tension all influence the final cable.
Material feeding
The process starts with the selected insulation or sheath material. Depending on the product specification, different polymer materials may be used. The feeding system should provide a stable supply to the extrusion unit. If feeding becomes irregular, the extrusion process may also become unstable.
Plasticizing and extrusion
Inside the extruder, the screw transports the material through heated zones. The material gradually becomes a workable melt. The screw geometry, temperature setting, material characteristics, and operating conditions all affect how the melt behaves.
We therefore do not treat temperature settings as universal numbers. A process suitable for one material may not be suitable for another. The final operating paraMeters should be determined during commissioning according to the actual material and cable specification.
Die forming
After the material is plasticized, it reaches the die. The die controls how the molten polymer is formed around the conductor or cable core.
This stage is important for insulation thickness and surface appearance. A suitable die design and stable extrusion process help produce a more consistent layer. The die should also be selected according to the cable size and material being processed.
Cooling and sizing
The newly formed cable is still hot and needs controlled cooling. Cooling helps the extruded layer stabilize its shape before the product moves to the next stage.
Cooling is not simply about making the cable cold as quickly as possible. The process needs to work together with extrusion speed, material behavior, product dimensions, and line layout. Poor coordination can affect surface quality or dimensional stability.
Traction and take-up
The traction system keeps the product moving through the line at a controlled speed. The take-up system then collects the finished cable onto the required reel or spool.
Stable traction and take-up are particularly important in continuous cable manufacturing. If line speed and take-up tension change too much, the finished product may not maintain the desired dimensions or winding condition.
3. Key Features of Our 80+100 Photovoltaic Extrusion Line
We design the 80+100 photovoltaic extruder production line around actual production needs. Instead of giving customers a fixed configuration that may not match their product, we first confirm the cable specifications, material requirements, expected capacity, equipment arrangement, and delivery schedule.
Two coordinated extrusion units
The 80+100 configuration combines two extrusion units with different nominal sizes. This provides a flexible equipment platform for photovoltaic cable processes that require coordinated extrusion stages.
The exact duty of each extruder depends on the customer's product. One unit may be assigned to a particular material or layer while the other handles another extrusion stage. We determine the configuration according to the actual process rather than simply matching a model name.
Continuous production design
Wire and cable manufacturing is normally a continuous process. Once the line is properly set up, material should move smoothly from feeding through extrusion, cooling, traction, and take-up.
Our focus is therefore on coordination between equipment sections. A production line should not only have capable individual machines; those machines need to work together.
Practical operation
Industrial equipment is operated by people every day. For this reason, we pay attention to practical operation, adjustment, maintenance access, and process monitoring.
A complicated system is not automatically a better system. In our view, operators should be able to understand the main production conditions and respond quickly when a process needs adjustment.
Configurable production line
Different photovoltaic cables have different structures and material requirements. We can discuss the configuration according to the customer's product specifications and production goals.
Possible configuration considerations include:
Extruder arrangement
Material feeding system
Die and tooling requirements
Cooling section
Traction system
Take-up equipment
Electrical control system
Line layout
Product inspection requirements
4. Technical Considerations for Photovoltaic Cable Production
A photovoltaic cable extrusion machine does not determine the final cable standard by itself. The cable is a complete product, and its performance depends on the conductor, insulation, sheath, material formulation, dimensions, process conditions, and final testing.
This point is worth making clearly because it is sometimes misunderstood during equipment purchasing. Buying a photovoltaic cable extrusion line does not automatically mean that the finished cable will meet a particular international standard. The production process and finished product still need to be developed and tested against the applicable specification.
For example, IEC 62930:2017 applies to certain single-core cross-linked insulated power cables with cross-linked sheath for the DC side of photovoltaic systems. The standard covers cables rated up to and including 1.5 kV DC and states a normal continuous maximum conductor temperature of 90°C, with a limited period at 120°C.
For cable conductors, IEC 60228:2023 specifies nominal cross-sectional areas from 0.5 mm² to 3,500 mm² for a wide range of electric power cables and cords, together with requirements concerning wire numbers, sizes, and resistance values. It covers solid, stranded, and Milliken conductors as well as certain flexible copper conductors.
For extruded power cables, IEC 60502-1:2021 specifies construction, dimensions, and test requirements for certain power cables with extruded solid insulation at rated voltages of 1 kV and 3 kV.
These standards are useful references when developing a cable production process, but the correct standard always depends on the final cable type and intended application.
Reference data for photovoltaic cable production
| Reference | Relevant Information | Why It Matters to Extrusion Production |
|---|---|---|
| IEC 62930:2017 | PV cables up to and including 1.5 kV DC; normal continuous maximum conductor temperature of 90°C | Helps define relevant cable construction and performance requirements |
| IEC 60228:2023 | Nominal conductor cross-sectional areas from 0.5 mm² to 3,500 mm² for covered cable types | Provides conductor-related reference information for cable design |
| IEC 60502-1:2021 | Construction, dimensions and testing requirements for certain extruded-insulation power cables | Provides a reference when developing applicable cable products |
Source: International Electrotechnical Commission (IEC) official publications. Applicability depends on the specific finished cable product.
Another useful consideration is insulation and sheath thickness. IEC 60811-201 provides methods for measuring insulation thickness for common insulating compounds, while IEC 60811-202 provides methods for measuring non-metallic sheath thickness.
From our equipment point of view, this means the extrusion process should provide enough control and stability to support the required product dimensions. The actual test method, acceptance criteria, and final product certification remain the responsibility of the cable manufacturer according to the applicable standard.
5. Production Parameters We Confirm Before Manufacturing
When a customer asks us for an 80+100 photovoltaic extrusion production line, we do not start by sending a generic quotation. We first ask what the customer wants to produce.
This is a very practical step. A line that works well for one photovoltaic cable may need a different configuration for another product.
| Item | Information We Confirm | Effect on Equipment Configuration |
|---|---|---|
| Product | Photovoltaic wire or cable type | Determines the general production process |
| Conductor | Material, structure and target dimensions | Influences product handling and process requirements |
| Insulation / Sheath | Material type and layer requirements | Influences extrusion and temperature control |
| Product Size | Target cable diameter and layer thickness | Influences die, cooling and line arrangement |
| Production Capacity | Expected output and working schedule | Influences line configuration and process coordination |
| Factory Layout | Available production space and equipment position | Influences line length and equipment arrangement |
We also discuss whether the customer needs additional take-up and unwinding equipment, auxiliary machines, specific control functions, or other production accessories.
Once these details are clear, we can prepare a more suitable equipment configuration. This approach is slower than simply copying a standard quotation, but it reduces the risk of buying equipment that does not fit the actual production requirement.
6. Applications of the 80+100 Photovoltaic Extruder Production Line
The main application of this line is photovoltaic wire and cable production. Solar power systems need cables that can operate in demanding outdoor conditions, and the cable construction has to match its intended electrical and environmental requirements.
Our extrusion equipment can be considered for different cable manufacturing applications, including:
Photovoltaic cables: production of cable insulation or sheath layers for solar power applications.
Solar wires: continuous extrusion processing for photovoltaic wire products.
DC-side solar cables: cable production processes designed for photovoltaic system connections.
Specialized wire products: extrusion applications where the customer requires coordinated multi-stage processing.
Other cable products: depending on the material, product dimensions, and line configuration.
Our company also manufactures equipment for automotive wires, electronic wires, network communication cables, charging pile cables, and other extrusion-related products. This broader experience is useful when customers need a production line that can be adapted to more than one product family.
Why solar cable production needs stable extrusion
Photovoltaic cables are often installed outdoors and may be exposed to heat, sunlight, moisture, mechanical stress, and other environmental conditions. The finished cable therefore needs to be manufactured according to its intended application and product specification.
From the equipment side, we focus on stable feeding, controlled extrusion, consistent forming, reliable cooling, and smooth take-up. These are basic things, but basic things are often what determine whether a production line is easy to operate day after day.
7. How We Manufacture and Test the Production Line
We treat manufacturing as a process rather than simply assembling machines together.
Before production begins, we confirm the customer's product specifications, material requirements, expected production capacity, equipment configuration, and delivery schedule. This information becomes the basis for equipment preparation and line assembly.
Step 1: Requirement confirmation
We discuss the product structure and production target with the customer. If the customer has drawings, material information, cable specifications, or existing production data, these details help us understand the application more accurately.
Step 2: Equipment configuration
We determine the extrusion units and supporting equipment according to the confirmed process. The 80+100 configuration is then integrated with the necessary feeding, forming, cooling, traction, take-up, control, and auxiliary systems.
Step 3: Manufacturing and assembly
Equipment components are manufactured and assembled according to the agreed configuration. Mechanical alignment, electrical connections, control components, and supporting systems all need to be checked during assembly.
Step 4: Line testing
Before shipment, the complete production line is assembled, tested, and inspected according to the agreed requirements. We use this stage to identify installation or coordination problems before the equipment reaches the customer's factory.
Step 5: Shipment preparation
After inspection, the equipment is prepared for transportation. We normally use moisture-resistant materials, protective cushioning, and strong export wooden cases or pallets. The packaging method is selected according to the equipment structure and transportation requirements.
This matters because a well-built production line still needs to arrive safely. Loading, handling, storage, and long-distance transportation can all create risks for industrial equipment if packaging is not properly planned.
8. Why Choose Wuxi Shuochuan for a Photovoltaic Extrusion Line?
There are many extrusion equipment suppliers in the market. For us, the important question is not simply whether we can provide an extruder. The more important question is whether we can understand the customer's production process and build a complete line around it.
Wuxi Shuochuan Electromechanical Equipment Manufacturing Co., Ltd. integrates R&D, manufacturing, and sales. We have obtained more than ten utility model patent certificates, reflecting our continued investment in equipment development and practical engineering improvements.
The company has also stated that it has passed ISO 19001 quality management system certification. For any customer requiring certification documentation, we recommend confirming the exact certificate number, scope, and applicable standard during the purchasing process.
Our product range covers high-speed extruders, three-in-one BV extrusion automatic production lines, three-in-one plus one BVVB automatic production lines, photovoltaic wire and Cable Production Lines, automotive Wire Production lines, electronic Wire Production Lines, network communication wire production lines, charging pile cable production lines, take-up and unwinding equipment, auxiliary equipment, and related raw materials.
This gives us a wider understanding of extrusion production. We are not only looking at one machine. We are familiar with the relationship between extrusion, cable forming, take-up, unwinding, and automated production.
Our working philosophy
We follow the principle of “Quality First, Continuous Improvement, and Honest Service.” In practical terms, that means we try to keep communication clear, equipment requirements realistic, and the production process understandable.
We also believe that equipment should be designed around the people who use it. A production line may contain advanced controls and mechanical systems, but operators still need to set parameters, monitor production, perform routine maintenance, and solve ordinary production issues.
That is why we place value on human-machine friendliness as well as equipment performance.
9. 80+100 Photovoltaic Extruder Production Line: What Buyers Should Compare
When comparing photovoltaic cable extrusion machines from different suppliers, we suggest looking beyond the extruder model. Two suppliers may both quote an “80+100 photovoltaic extrusion line,” but the actual equipment configuration can be quite different.
| Comparison Point | What to Ask the Supplier | Why It Matters |
|---|---|---|
| Extruder Configuration | What is the function of each extrusion unit? | Different cable structures require different processing arrangements |
| Material Compatibility | Which materials have been considered for the process? | Material behavior affects temperature and extrusion conditions |
| Die System | Is tooling selected according to the target cable size? | Die design directly affects forming quality |
| Cooling | How is the cooling section arranged? | Cooling affects product shape and dimensional stability |
| Traction | How is line movement controlled? | Stable traction supports consistent production |
| Take-Up | What winding method is included? | Proper take-up is important for continuous cable production |
| Testing | What inspection is completed before shipment? | Pre-shipment testing helps identify installation problems early |
| After-Sales Support | What technical documents and support are provided? | Useful documentation makes installation and operation easier |
For us, a good quotation should explain what is included instead of only showing one total price. The customer should understand the extrusion units, auxiliary equipment, control system, take-up and unwinding equipment, technical documents, accessories, and other agreed items.
10. Frequently Asked Questions About the 80+100 Photovoltaic Extruder Production Line
What does 80+100 mean in this photovoltaic extrusion line?
In general, 80+100 indicates two extrusion units with different nominal extruder sizes. The exact function of each unit depends on the cable structure, material, and production process. We confirm the detailed configuration with the customer before manufacturing.
What products can the 80+100 line produce?
The line is primarily intended for photovoltaic wire and cable extrusion applications. Depending on the selected configuration and materials, it can also be considered for other extrusion-related products. Final suitability should be confirmed according to the actual product specification.
Can the production line be customized?
Yes. We can discuss customization according to product dimensions, materials, production capacity, equipment layout, take-up requirements, auxiliary equipment, and other manufacturing conditions.
What materials can be processed?
The applicable material depends on the final product and extrusion configuration. We recommend providing the material grade or technical data before equipment selection so that the extrusion system, temperature control, die, and supporting equipment can be considered correctly.
Does the line automatically guarantee IEC-compliant photovoltaic cables?
No. The production line is manufacturing equipment. Whether the finished cable meets IEC 62930 or another applicable standard depends on the complete cable design, materials, process parameters, dimensions, testing, and conformity requirements. IEC 62930:2017 defines requirements for a specific category of photovoltaic cables, so the applicable standard should always be checked against the final product.
How long does production take?
Lead time normally depends on the extruder model, line configuration, customization requirements, and order quantity. We confirm the expected delivery schedule with the customer before production.
What is included in standard delivery?
Standard delivery generally includes the complete extruder production line, necessary components, technical documents, accessories, and other items specified in the order. The exact supply scope is confirmed in the contract or technical agreement.
How is the equipment shipped?
We can arrange transportation by sea, air, or land depending on the destination, equipment size, and delivery schedule. Industrial equipment is normally protected with moisture-resistant materials, cushioning, wooden cases, or pallets as appropriate.
What payment terms do you accept?
Payment terms are normally arranged according to the contract. A common arrangement includes a deposit before production and the balance before shipment, although the final terms depend on the agreed order.
11. A Practical Approach to Your Photovoltaic Cable Production Project
If you are looking for an 80+100 photovoltaic extruder production line, we recommend starting with the product rather than the machine.
Tell us what photovoltaic wire or cable you plan to produce, the conductor structure, insulation and sheath materials, target dimensions, expected production capacity, and available factory space. If you already have a product drawing, technical specification, or existing production data, that information can make the discussion much more precise.
We can then evaluate the extrusion arrangement, supporting equipment, cooling section, traction system, take-up system, control requirements, and other line components.
Our goal is not simply to supply an 80+100 extrusion machine. We want to provide a complete and workable photovoltaic Cable Extrusion Production Line that fits the customer's actual manufacturing process.
For a photovoltaic cable manufacturer, stable production is built from many small things working together: steady material feeding, suitable extrusion conditions, accurate forming, controlled cooling, reliable traction, proper take-up, and clear operation. When these parts are properly coordinated, the production line becomes much easier to manage.
That is the approach we take at Wuxi Shuochuan: understand the application first, configure the equipment carefully, test the complete line before shipment, and continue improving the equipment based on real manufacturing needs.
Contact us to discuss your 80+100 Photovoltaic Extruder Production Line project, product specifications, material requirements, production capacity, and customized equipment configuration.



 WhatsApp
 телефон